How to Inspect Carbon Steel Flanges for Damage?
Carbon steel flanges are widely used to connect pipes, valves, equipment, and other components in industrial piping systems. As a flange needs to provide both a mechanical connection and a sealing function, damage that seems relatively small on visual examination may occasionally take on a more serious connotation once the component is mounted and exposed to pressure, temperature variations, vibration, or repetitive maintenance. This means that an examination should not only check for visible corrosion or dents, but also evaluate the flange size, sealing surface, bolt hole arrangement, material quality, and other indicators that need non-destructive testing. The inspection technique should be adopted according to the flange type, material, service circumstances, relevant standard, and project requirements. For example, ASME B16.5 provides pressure-temperature ratings, materials, dimensions, tolerances, marking, and testing for pipe flanges and flanged fittings in the range of sizes specified. ASME B16.47 covers large diameter steel flanges from NPS 26 to NPS 60. Therefore, a productive inspection procedure begins with the relevant technical documentation, and then integrates visual examination, dimensional verification, and NDT if required.
Start With the Flange Identification and Inspection Criteria
Before looking at a flange, identify the component you are inspecting and the requirements that relate to that component. Identify the flange size, pressure class or rating, material grade, facing type, manufacturing specification, and necessary drawing or purchasing specification first. Without this information, a measurement cannot always be classified as either acceptable or unsuitable, as dimensions and tolerances are dependent on the relevant flange standard and design criteria.
Inspection of a new flange may be performed based on the purchase specification, drawing, material documents, and appropriate manufacturing standard. If a flange is already in a pipe system, the examination should include service history, prior repairs, corrosion exposure, operating circumstances and the purpose for the inspection. For example, a flange in a corrosive process may need more consideration for localised metal loss than a comparable component in a relatively moderate environment.
The first stage is commonly missed since the inspector’s tendency is to begin by determining the physical condition of the component. But the reference standards specify what really should be measured and which sort of flaw is most important.
Examine the Flange Face and Sealing Areas Closely
Look for Damage That Could Affect Gasket Contact
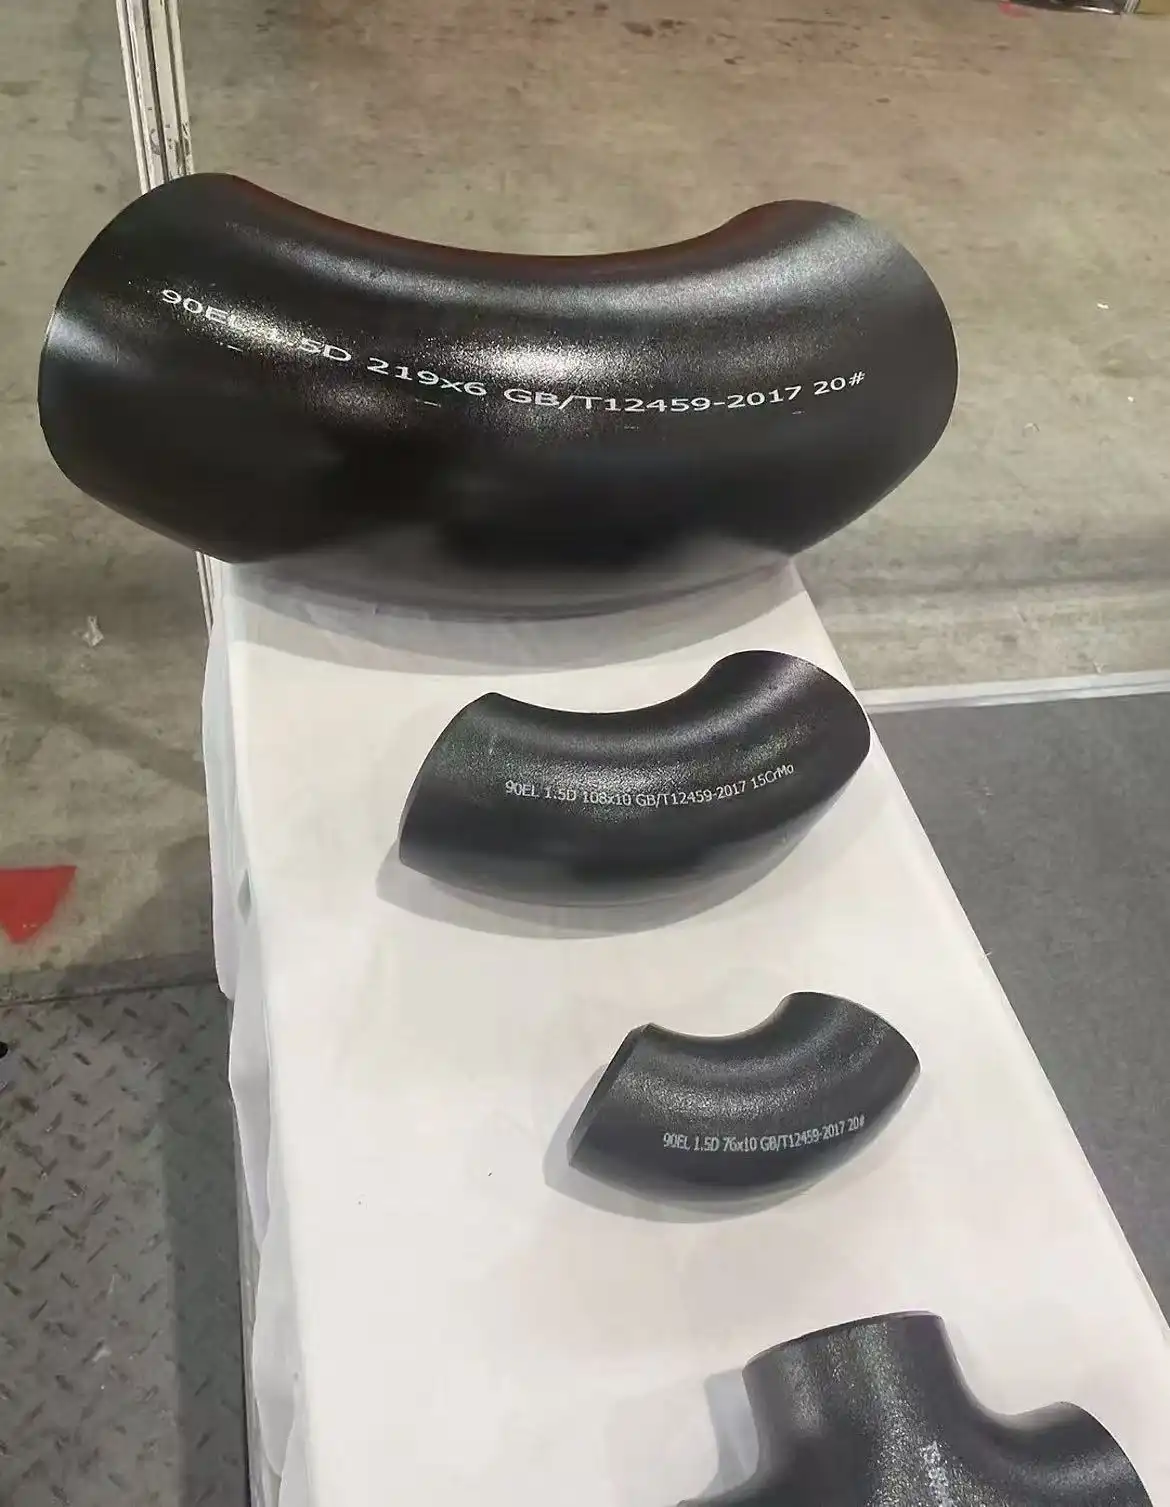
Particular care should be paid to the flange face, as its quality directly influences the contact between the flange and the gasket. Inspect the whole sealing area for scratches, dents, gouges, corrosion, pitting, implanted foreign material, and other anomalies. Surface damage should not be evaluated by sight alone. The site, depth, direction, and the connection to the sealing region are also essential.
A minor surface mark outside the functional sealing area may not mean the same as a deep groove that cuts across the gasket contact region. Similarly, localised pitting corrosion should be examined more closely than uniform surface discolouration.
Clean the surface prior to reaching a final determination, as minor indicators might be hidden by rust scale, old gasket material, paint, dirt, or process deposits. Usually, enough illumination is sufficient for a preliminary check, and magnification might be helpful if the surface quality is not easy to judge visually.
Inspect Bolt Holes, Outside Edges, and Transition Areas
But it is not just the sealing face that must be paid attention to. Check for any deformation of the bolt holes, enlarged apertures, burrs, cracking, or localised corrosion. Also inspect the outer edge and transition regions for dents and impact marks.
Special attention should be paid to places where geometry changes or mechanical stresses may be focused. If the flange shows apparent cracking, significant corrosion, or deformation, the examination should go beyond a basic visual evaluation, rather than assuming that the surface appearance reflects the whole state of the component.
Carbon steel parts, including Carbon steel flanges, may also be affected by uneven corrosion. Localised pitting may lower the material thickness across a short region, yet the flange may seem to be generally sound. That is why visual examination is best used as the initial step in an inspection process, not as the only inspection approach.
Verify Dimensions Against the Applicable Standard
Measure Thickness and Overall Dimensions
Dimensional examination helps to see whether a flange is still in the appropriate geometry. Measure flange thickness at many areas, rather than relying on a single reading. Localised metal loss, machining variation, or deformation that may not be apparent from a broad visual inspection may be identified by several measurements.
Outside diameter and other significant dimensions should be verified against appropriate drawing or flange standard. For example, ASME B16.5 sets dimensions and tolerances for covered pipe flanges and flanged fittings; therefore, inspectors should compare actual measurements with the criteria pertaining to the particular flange, rather than with a general dimensional value.
Dimensional changes may be particularly valuable when evaluated against past inspection data for an in-service flange. One measurement gives information about the current state, and many measurements may offer information about the change of the component over time.
Check Bolt-Hole Size and Orientation
The bolt holes should suit the planned bolting layout and not induce any unwanted alignment or loading issues. The inspector shall ensure that the hole diameter, bolt-circle arrangement, number of holes, and their relative location to each other conform to the applicable flange standard.
Check for lengthy holes, local deformation, excessive burrs, or corrosion on the margins of holes. If the flange has been built and disassembled frequently, mechanical deterioration surrounding the bolt holes might be more than just discolouration on the surface.
It is also crucial to differentiate between production dimensions and damage-related dimensional changes. A measurement that does not match a drawing does not always mean the flange has deteriorated. The examination should determine whether the discrepancy is because of manufacturing tolerance, measurement ambiguity, design variance, or real service damage.
Evaluate Flatness and Alignment of the Mating Surfaces
Check flatness and alignment if there is evidence of distortion, poor gasket contact, installation difficulties, or mechanical damage. A straightedge and feeler gauge may give a useful first check, and if tighter dimensional control is necessary, more accurate measurement equipment may be acceptable.
The aim here is not just to come up with a number but to see whether the flange shape is still adequate for the connection it is designed to serve. A flange which has been bent by impact, overtightening, heat effects or other mechanical stresses may need further technical review before re-use.
The relationship of the surfaces should also be checked when two mated flanges are checked. When pipe has been relocated, or equipment nozzles have gotten misaligned, an issue with alignment may not be caused by a single flange.
Use NDT When Visual and Dimensional Checks Are Not Enough
Visual and dimensional inspections can identify many common forms of damage in Carbon steel flanges, but they cannot reliably reveal every discontinuity. NDT becomes useful when the service history, material condition, suspected defect, or inspection specification indicates that a deeper examination is necessary.
The method should be selected according to the suspected defect and the material. No single NDT technique is appropriate for every type of flaw. More importantly, finding an indication is not the same as determining that a flange is unacceptable. Acceptance criteria normally come from the applicable code, standard, engineering specification, or purchase requirement.
Use Magnetic Particle Testing for Surface and Near-Surface Cracking
Magnetic particle testing is particularly useful for carbon steel and other ferromagnetic materials when surface or near-surface discontinuities are suspected. ASTM E709 describes magnetic particle examination as a method for detecting cracks and other discontinuities at or near the surface of ferromagnetic materials. The standard also notes that indications need to be interpreted and evaluated against a separate code, specification, or agreement defining what is unacceptable.
For a carbon steel flange, areas around bolt holes, transitions, machined surfaces, and locations with suspected cracking can be examined using an appropriate magnetic particle procedure. The surface normally needs to be prepared so that contaminants do not interfere with the examination.
The result should be documented rather than described simply as “passed” or “failed.” The location, orientation, appearance, and relevant characteristics of indications should be recorded, followed by evaluation against the applicable acceptance criteria.
Consider Ultrasonic Testing for Volumetric Examination
Ultrasonic testing can provide information about discontinuities below the surface and can also be used for thickness measurements when the appropriate procedure and equipment are selected. The technique is based on transmitting sound energy into the material and analyzing returned signals.
However, the inspection procedure should match the component being examined. ASTM E213, for example, is specifically a practice for ultrasonic testing of metal pipe and tubing, and its scope should not be treated as a universal acceptance procedure for every flange configuration. This distinction is important when preparing an industrial inspection procedure because component geometry, thickness, access, surface condition, and the suspected defect all influence the suitability of a particular UT technique.
For in-service carbon steel flanges, ultrasonic examination can be particularly useful when there is concern about localized metal loss or internal discontinuities that cannot be assessed adequately through visual inspection alone. The inspection report should identify the procedure used, examined areas, measured values or indications, and the applicable acceptance requirements.
Apply Radiographic Testing When Internal Imaging Is Required
Radiographic testing uses X-rays or gamma radiation to produce an image that can reveal variations within a component. It can be useful when the inspection objective requires radiographic examination and the component geometry and project requirements make the technique appropriate.
ASTM E1742/E1742M establishes minimum requirements for radiographic examination of metallic and nonmetallic materials, including applications involving Carbon steel flanges, and addresses factors such as image quality and examination control. The current ASTM listing identifies E1742/E1742M-23 as the active version.
Radiographic examination should be performed under a qualified procedure because exposure conditions, image quality, coverage, and interpretation all affect the reliability of the examination. Radiation safety requirements must also be controlled by appropriately qualified personnel.
For most routine flange inspections, RT should not simply be presented as a mandatory step. Its use depends on the component, suspected discontinuity, accessibility, applicable specification, and project inspection requirements.
Assess Corrosion and Metal Loss in Service
Distinguish Surface Rust From Localized Material Loss
Carbon steel flanges exposed to moisture, chemicals, salt-containing environments, or process conditions can develop corrosion over time. Surface rust does not automatically mean that a flange has reached an unacceptable condition, but corrosion that has produced pitting or measurable metal loss deserves closer attention.
Inspectors should therefore distinguish between superficial corrosion products and actual loss of base metal. Cleaning followed by visual examination can help establish the extent of the condition, while thickness measurement may be appropriate where localized loss is suspected.
The location of corrosion also matters. Metal loss on a noncritical external area may need a different assessment from metal loss affecting the sealing surface, bolt-hole region, or a highly stressed section of the flange.
Pay Attention to Pitting and Localized Damage
Pitting deserves particular attention because it can be deeper than its surface appearance suggests. Instead of describing a corroded flange simply as “rusty,” inspection records should identify where the corrosion occurs and whether measurable material loss is present.
Where the remaining thickness or structural condition is uncertain, additional measurement or engineering evaluation may be required. The decision to repair, re-machine, replace, or continue using the flange should be based on the applicable design and acceptance requirements rather than on visual judgment alone.
Conclusion
Inspecting carbon steel flanges for damage requires more than a quick visual check. A reliable approach begins by confirming the applicable flange standard and inspection criteria, followed by a detailed examination of the sealing surface, bolt holes, outside edges, and other areas where damage or corrosion may develop. Dimensional checks can then determine whether thickness, diameter, bolt-hole arrangement, flatness, and alignment remain within the applicable requirements.
When surface or internal conditions cannot be evaluated adequately through routine inspection, appropriate NDT methods can provide additional information. Magnetic particle testing is suited to surface and near-surface discontinuities in ferromagnetic materials, while ultrasonic and radiographic methods can be selected for different examination objectives and component conditions. The important point is that each method should be used under a suitable procedure and interpreted against the relevant acceptance criteria.
A well-documented inspection process also creates a useful history for future maintenance. By recording measurements, visible conditions, NDT results, and the standards or specifications used for evaluation, engineers and maintenance teams can make better-informed decisions about continued service, repair, or replacement of the flange. For more information or assistance with carbon steel flange inspections, please contact us at oudi-04@oudiguandao.com.
FAQ
1. How often should carbon steel flanges be inspected?
The frequency of inspections depends on the operating conditions and criticality of the system. Generally, it's recommended to perform visual inspections annually and more comprehensive NDT inspections every 3-5 years or as specified by industry standards.
2. Can surface corrosion on a carbon steel flange be repaired?
Minor surface corrosion can often be addressed through cleaning and reapplication of protective coatings. However, severe corrosion may require flange replacement to ensure system integrity.
3. What are the most common types of damage found in carbon steel flanges?
Common types of damage include surface scratches, dents, corrosion, cracks, and dimensional deviations due to wear or improper handling.
4. Is it necessary to use all NDT techniques when inspecting carbon steel flanges?
Not always. The choice of NDT techniques depends on the specific requirements of the inspection, the flange's criticality, and any known or suspected issues.
References
1. Smith, J. A. (2018). "Comprehensive Guide to Carbon Steel Flange Inspection Techniques." Journal of Industrial Maintenance, 42(3), 156-172.
2. Johnson, R. B., & Thompson, L. M. (2019). "Non-Destructive Testing Methods for Metallic Flanges in Process Industries." NDT International, 85, 23-37.
3. Brown, C. D. (2017). "Best Practices for Visual Inspection of Carbon Steel Piping Components." Plant Engineering Quarterly, 29(2), 45-58.
4. Davis, E. F., & Wilson, G. H. (2020). "Dimensional Verification Techniques for Industrial Flanges." Metrology and Measurement Systems, 27(1), 81-96.
5. Anderson, K. L. (2016). "Corrosion Detection and Prevention in Carbon Steel Flange Assemblies." Corrosion Science and Technology, 51(4), 312-328.
6. Lee, S. Y., & Patel, R. K. (2021). "Advanced Ultrasonic Testing Methodologies for Flange Integrity Assessment." Materials Evaluation, 79(5), 567-582.
Need help finding the right solution with our experts. Please contact us.

SINCE 1998 Your Reliable Pipeline Manufacturer



